Product Overview
The Underground Mine Drainage Automation System automatically detects sump water levels and other parameters, building mathematical models based on water level and mine electricity usage patterns to control water pumps in rotation. The system achieves peak-shaving and valley-filling energy optimization while enabling unattended pump room operation and safe, reliable equipment performance.
Product Description
Underground water accumulation is a persistent and serious hazard in coal mining. Effective drainage is essential not only for production continuity but for the prevention of catastrophic flooding incidents. The Underground Mine Drainage Automation System transforms traditional manually-operated pump rooms into intelligent, self-managing facilities that optimize energy consumption while maintaining rigorous safety standards.
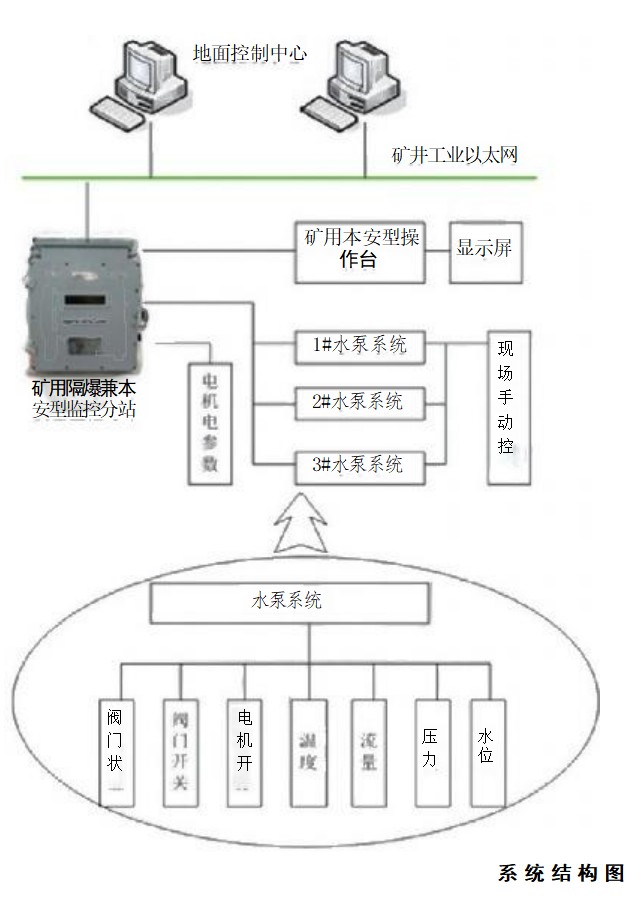
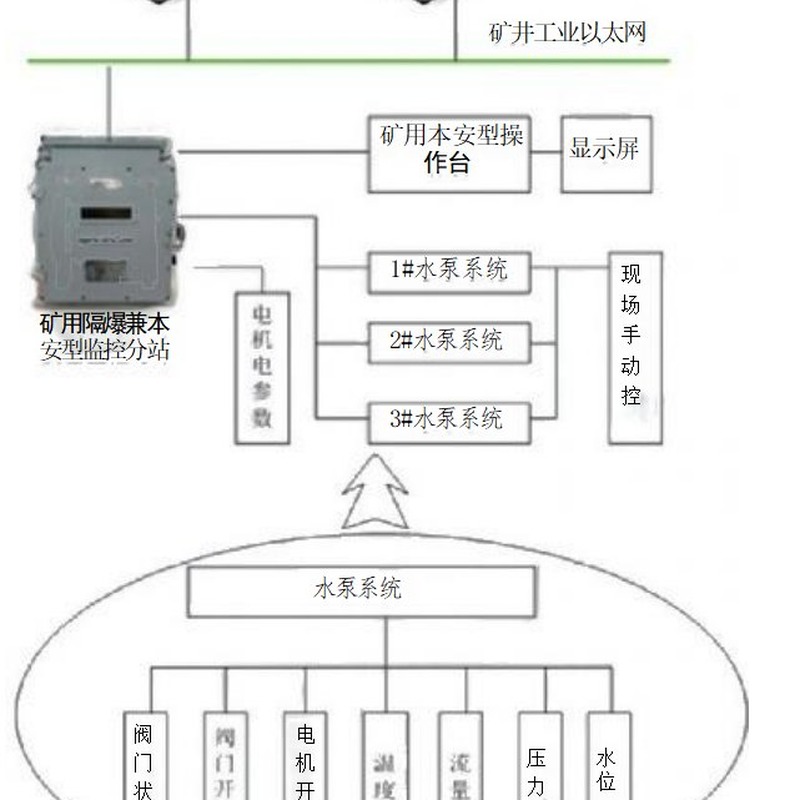
The system's control core is a mining-grade PLC that integrates data from a comprehensive sensor suite including status sensors, electrical parameter sensors, PT100 temperature sensors, flow sensors, pressure sensors, and liquid level sensors. This multi-dimensional sensing capability enables the system to build sophisticated mathematical models that account for sump water level, inflow rate, electricity grid load, and peak/valley pricing periods — automatically determining optimal pump start/stop timing to minimize energy costs while ensuring water levels remain within safe parameters.
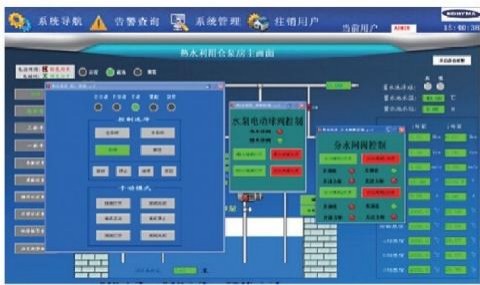
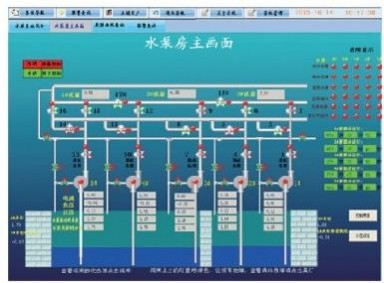
The system supports three operating modes: surface full-automatic control, local manual control, and local program control, providing operational flexibility for both routine and emergency scenarios. Intelligent scheduling algorithms automatically detect water level rise rates, estimate inflow volume, and dynamically adjust the number of active pumps — starting additional pumps during high-inflow events and shutting down excess capacity during low-flow periods. The peak-shaving functionality leverages grid load and peak/valley electricity pricing to schedule pump operations during low-cost periods, generating significant energy savings.
Video linkage functionality enables automated camera switching based on operations and fault events, providing visual verification of pump room conditions. Audio capabilities include voice alerts during equipment start/stop and fault conditions, plus surface-to-underground broadcast intercom. A rail-mounted mobile camera enables remote visual inspection of the entire pump room. The system's layered distributed architecture encompasses sensing, control, communication, and monitoring layers, with communication via industrial Ethernet (fiber ring network), Profibus, and Modbus protocols, plus Wi-Fi and 4G/5G private network options (requiring explosion-proof certification).
Key Features
- Three operating modes: surface full-automatic, local manual, local program control
- Image linkage: automated camera switching based on operations and faults
- Audio alerts and surface-to-underground broadcast intercom
- Peak-shaving energy optimization based on grid load and pricing periods
- Intelligent inflow estimation with dynamic pump count adjustment
- Rail-mounted mobile camera for remote pump room inspection
- Layered distributed architecture: sensing, control, communication, monitoring
Technical Specifications
| Parameter | Value |
|---|
| Control Core | Mining-grade PLC |
| Sensor Types | Status, electrical, temperature (PT100), flow, pressure, liquid level |
| Communication Network | Industrial Ethernet (fiber ring), Profibus, Modbus |
| Communication Methods | Wi-Fi, 4G/5G private network (explosion-proof required) |
Applications
Underground coal mine drainage pump room automation control, mine safety production management, unattended pump room operation, and flood prevention management.
![]()
![]()
![]()