Product Overview
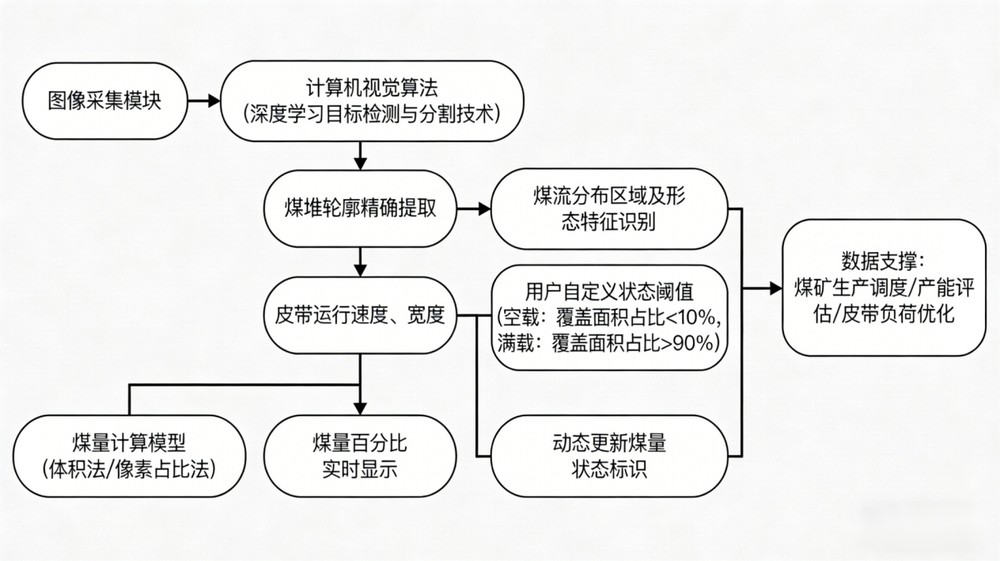
The Mining Coal Quantity Recognition & Monitoring Device monitors coal quantity on belt conveyors using intelligent image-recognition technology, developed for smart-mining construction. Two intrinsically safe image-processing cameras act as the eyes of the device, capturing underground transport scenes such as coal flow on conveyors.
Product Description
Accurate measurement of how much coal is moving on each conveyor supports belt load balancing, production accounting and efficient speed control — key goals of smart-mining construction. The Mining Coal Quantity Recognition & Monitoring Device was developed for exactly this purpose: it monitors coal quantity on belt conveyors using intelligent image-recognition technology instead of conventional weighbridges or belt scales.
The device's main system structure and composition follow the original material. Its "eyes" are two intrinsically safe image-processing cameras that capture underground transport scenes such as the coal flow on conveyors. The cameras feed images to the recognition engine, which analyzes the visual profile of the coal on the belt and derives a quantitative estimate of the load, including variations in flow as the conveyor operates.
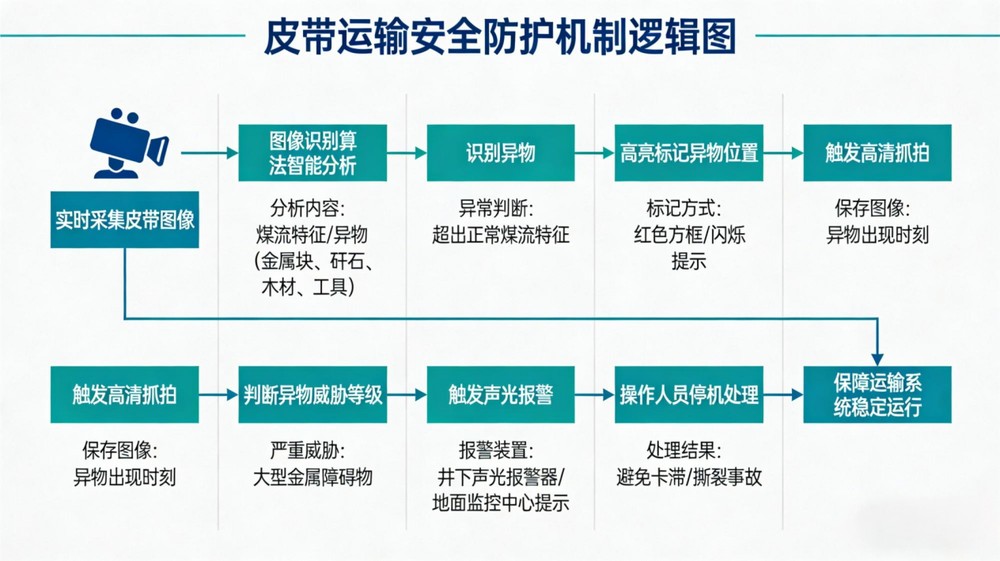
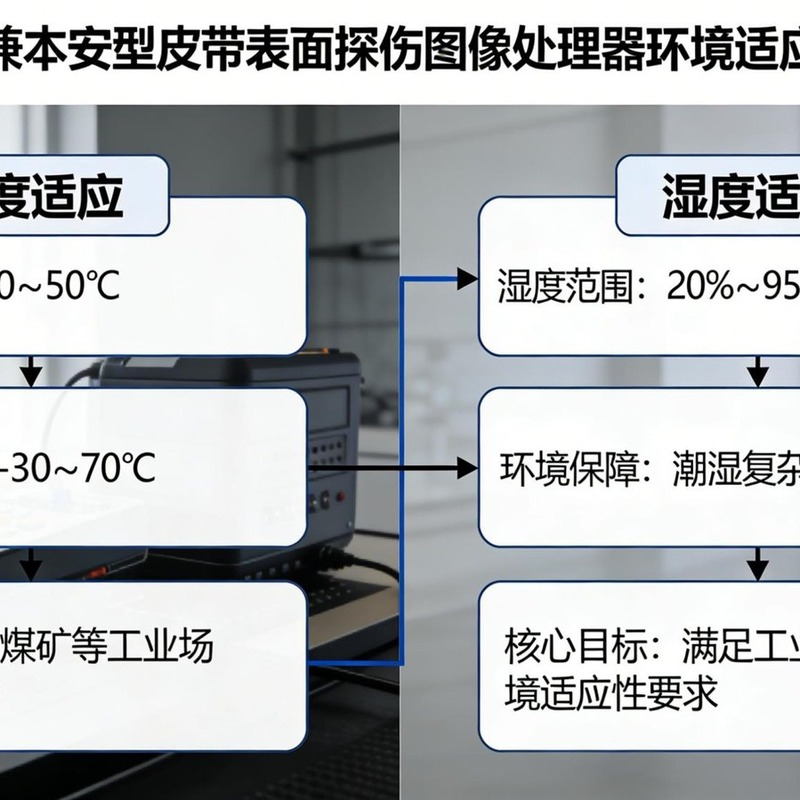
The intrinsically safe design ensures safe use in explosive environments containing mine gas, so the cameras and processing can be installed directly above belt lines in hazardous underground areas. By combining vision-based recognition with mine safety certification, the device gives mines a practical, non-contact method for coal quantity monitoring that integrates naturally into intelligent mining systems.
Key Features
- Coal quantity monitoring on belt conveyors
- Intelligent image-recognition technology
- Developed for smart-mining construction
- Two intrinsically safe image-processing cameras
- Visual capture of coal flow on conveyors
- Safe use in explosive environments containing mine gas
Technical Specifications
| Parameter | Value |
|---|
| Measurement Technology | Intelligent image recognition |
| Sensor Configuration | Two intrinsically safe image-processing cameras |
| Monitored Scene | Coal flow and quantity on belt conveyors |
| Safety Design | Intrinsically safe for gas environments |
| Application | Smart mining construction |
Applications
Belt conveyor coal quantity monitoring, mine production accounting, conveyor load management, and intelligent mining systems.
![]()
![]()
![]()