Coal Mine Gas Drainage Monitoring System | Pump Station Automation

Mine-wide gas drainage monitoring system with real-time pipeline and pump-station parameter monitoring, enabling unattended operation with inspection for safer gas management.
Category :

Product Overview

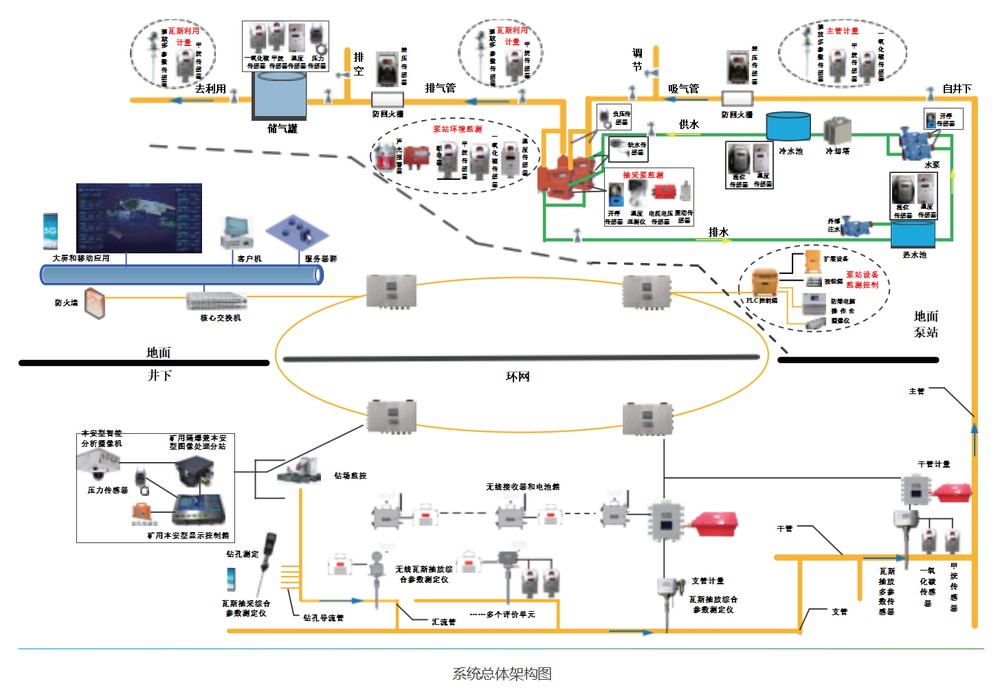
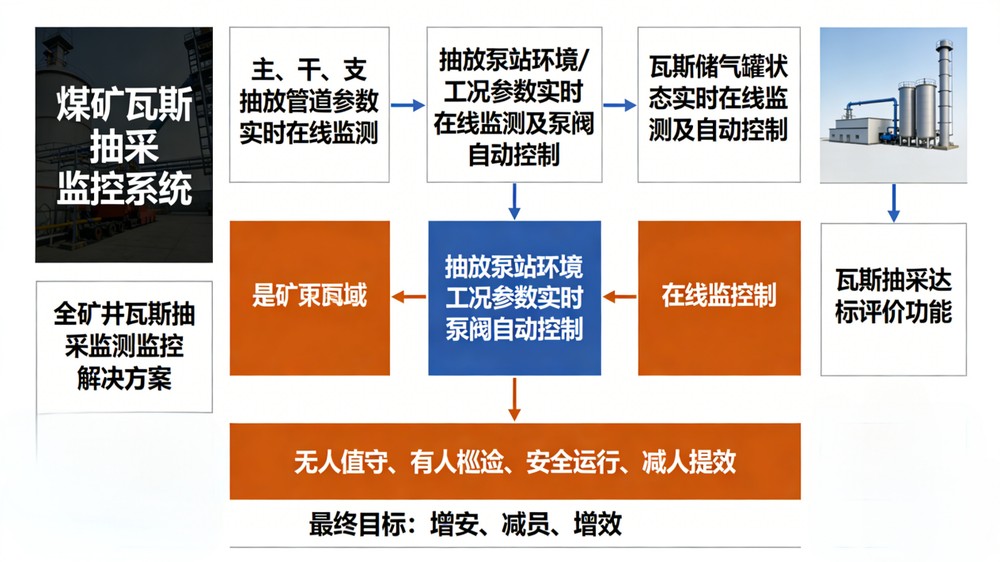
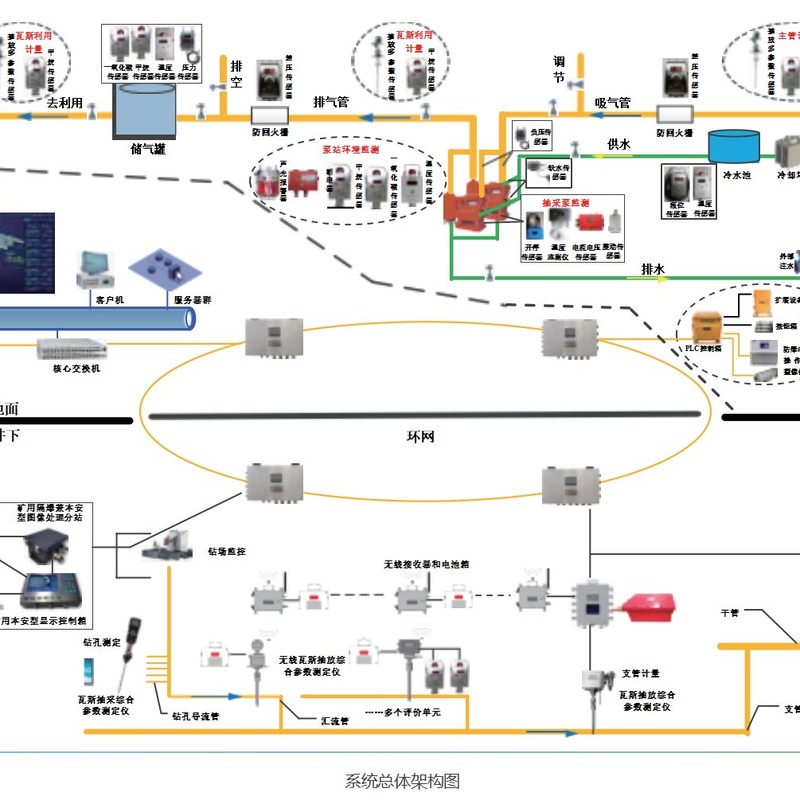
The Coal Mine Gas Drainage Monitoring System is a complete mine-wide solution for gas drainage monitoring, providing real-time online monitoring of main, branch and auxiliary drainage pipeline parameters as well as pump-station environment and operating parameters. It enables gas drainage pump stations to move toward unattended operation with inspection, improving safety and manpower efficiency.

Product Description

Gas drainage is one of the most important safety activities in gassy coal mines, and its effectiveness depends on continuous knowledge of what is flowing through every pipeline and how the pump stations are performing. This system provides complete mine-wide gas drainage monitoring, covering main, branch and auxiliary drainage pipeline parameters as well as the environment and operating parameters of every pump station.

Real-time online monitoring means discharge volume, concentration, negative pressure, temperature and related parameters along the drainage network are continuously visible to the control room. Because the system handles monitoring, control and data transmission as distinct, well-organized sections, it can be configured to match the mine's drainage network topology — main lines, branch lines and auxiliary lines each receive the appropriate instrumentation.

By turning manual reading rounds into continuous automated monitoring, the system allows gas drainage pump stations to move toward unattended operation with inspection rather than permanent staffing. Personnel are freed from repetitive reading tasks, abnormal states are detected immediately instead of at the next inspection round, and the mine gains a historical record of drainage performance for analysis, reporting and regulatory compliance.

Key Features

  • Complete mine-wide gas drainage monitoring solution
  • Real-time online monitoring of main, branch and auxiliary pipeline parameters
  • Pump-station environment and operating parameter monitoring
  • Integrated monitoring, control and data transmission sections
  • Enables unattended operation with inspection for pump stations
  • Immediate detection of abnormal drainage conditions
  • Historical drainage data for analysis and compliance

Technical Specifications

ParameterValue
Monitoring ScopeMain, branch and auxiliary drainage pipelines plus pump stations
Parameter TypesPipeline flow/concentration/pressure and station environment/operation
System SectionsMonitoring, control, data transmission
Operation ModelUnattended operation with inspection
ApplicationUnderground coal mine gas drainage

Applications

Coal mine gas drainage networks, pump-station automation, gas safety monitoring, and mine gas management compliance.

Related Products

Belt Surface Flaw Detection Image Processor | Flameproof Intrinsically Safe

Belt Surface Flaw Detection Image Processor | Flameproof Intrinsically Safe

Flameproof and intrinsically safe belt surface flaw detection image processor for real-time detection of bulges, peeling, cracking, tearing, edge wear and belt-joint abnormalities, AC 127 V.

Environmental Monitoring System for Metal & Non-Metal Mines

Environmental Monitoring System for Metal & Non-Metal Mines

Four-module environmental monitoring system for metal and non-metal mines — safety monitoring, precise personnel positioning, wireless communication and emergency broadcasting with 2-hour UPS backup.

Mining Design Assistance System | 2D/3D CAD Mine Design Software

Mining Design Assistance System | 2D/3D CAD Mine Design Software

CAD-based mine design assistance system with GIS and 3D GIS technology for roadways, sections and intersections, integrating 2D and 3D design inside CAD for coal-mine engineers.

Flameproof Solenoid Valve | Explosion-Proof Mining Valve

Flameproof Solenoid Valve | Explosion-Proof Mining Valve

Flameproof solenoid valve with AC electromagnet drive for automatic one-way control of water and non-corrosive liquids in mines and other gas-risk environments.

Flameproof Reversible Vacuum Magnetic Starter | 1140V Mining Motor Control

Flameproof Reversible Vacuum Magnetic Starter | 1140V Mining Motor Control

Flameproof reversible vacuum magnetic starter for 380/660/1140 V mine motors up to 200 A, with local/remote control and overload, short circuit, phase-loss and leakage protection.

Flameproof Intrinsically Safe Vacuum Feeder Switch | 1140V Mining

Flameproof Intrinsically Safe Vacuum Feeder Switch | 1140V Mining

Flameproof and intrinsically safe vacuum feeder switch for 1140 V/660 V mine networks up to 1000 A, with undervoltage, overload, short circuit and selective leakage protection.

Flameproof Intrinsically Safe Mining Speaker | Hi-Fi Underground Audio

Flameproof Intrinsically Safe Mining Speaker | Hi-Fi Underground Audio

Flameproof and intrinsically safe mining speaker with an imported high-power stereo hi-fi amplifier chip for clear voice and alarms in roadways, rest rooms and parking areas.

Flameproof Intrinsically Safe Mining Lithium Battery Power Supply

Flameproof Intrinsically Safe Mining Lithium Battery Power Supply

Flameproof and intrinsically safe lithium battery power supply for underground coal mines, with automatic fast switchover and certified safe operation in gas and coal-dust environments.

0
Inquire for more cooperation or product information.
We will contact you within 1 working day, please check your email.
Coal Mine Gas Drainage Monitoring System | Pump Station Automation
Name
Mail
Mobile phone (Optional)
Message
Send

PengXiang

We reply immediately
Welcome to our website. Ask us anything 🎉

Start Chat with: